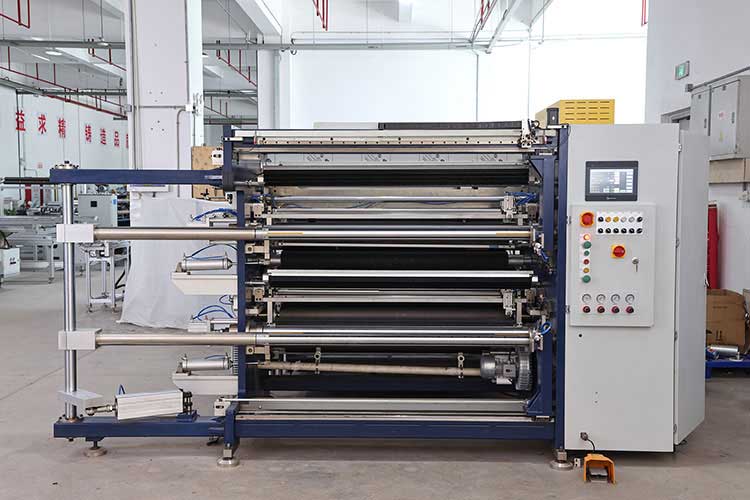
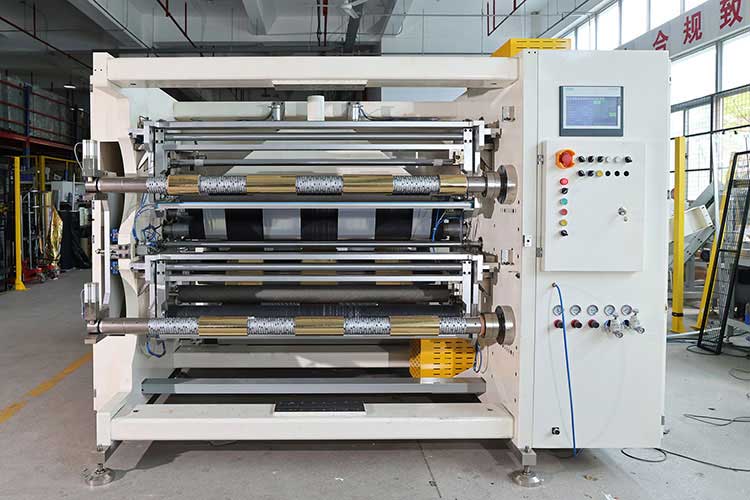
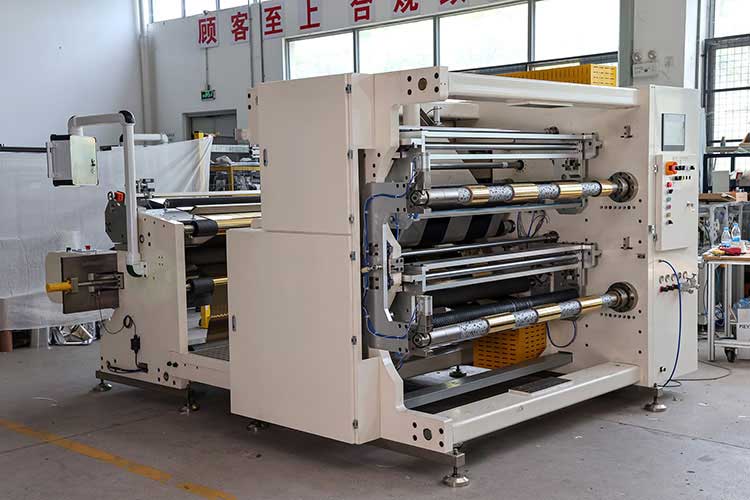
In the process of using the slitting machine, if the equipment parameters meet the standards but the actual effect is not good, it is likely to encounter the trap of "pseudo-high-end". This phenomenon usually stems from the fact that suppliers cover up actual performance defects by stacking theoretical parameters, which need to be systematically investigated and solved from the following aspects:
First, diagnosis of core parameters and process matching
1. Tension control system verification
• Check whether the theoretical tension range (e.g., 5-50N) matches the material properties
• Measured tension fluctuation value at different speeds (recommended ± within 0.5N)
• Verify the response time of the correction system (should ≤ 50ms)
2. Cutting accuracy decomposition test
• Tested at maximum design speed (e.g. 300m/min):
◦ Longitudinal slitting deviation (should ≤± 0.1mm)
◦ Diagonal error (should be ≤ 0.15mm/m)
• Check the radial runout of the tool (should ≤ 0.01mm)
Second, concealment performance trap investigation
1. Power system continuity test
• Detection after 8 hours of continuous full load operation:
◦ Spindle temperature rise (should ≤ 40°C)
◦ Velocity volatility (should ≤ 0.5%)
2. Control system response test
• Loss of positioning accuracy after emergency stop and restart (should ≤ 0.05mm)
• System response delay during specification switching (should ≤ 3 cycles)
Third, material suitability verification matrix
Create a material-parameter correspondence table for cross-testing:
| Material type | Best Tension (N) | Applicable knife types | Upper Speed (m/min) |
| PET film | 12-18 | Double-edged knife | 250 |
| Copper foil | 8-12 | Fillet knife | 180 |
| Non-woven fabric | 5-8 | Single-edged knife | 350 |
Fourth, solution implementation path
1. Parameter Optimization Process:
Material Testing → Build process libraries → Set parameter packages → Automatic matching
2. Hardware Upgrade Suggestions:
• Laser rangefinder (accuracy 0.001mm)
• Upgraded servo motor (overload capacity ≥150%)
• Configure temperature compensation system
3. Key points of supplier evaluation:
• Request for third-party test reports (e.g. EMC test data from CE certification)
• On-site inspection of the production site of equipment of the same specification
• Verify the original factory certification documents of core components
Fifth, effect verification standards
1. Qualified Output Criteria:
• First article pass rate ≥99.5%
• Scrap rate ≤0.3%
• Switching loss ≤ 1.5m
It is recommended to establish a CPK evaluation system for equipment capability index, which requires CPK ≥ 1.67 under stable working conditions. At the same time, a vibration analyzer is introduced to detect whether the natural frequency of the equipment resonates with the operating frequency, which is a common hidden reason for the parameters to meet the standards but the effect is poor. Through systematic verification, the problem of false parameter standards can be effectively identified to ensure that the real performance of the equipment meets the production needs.
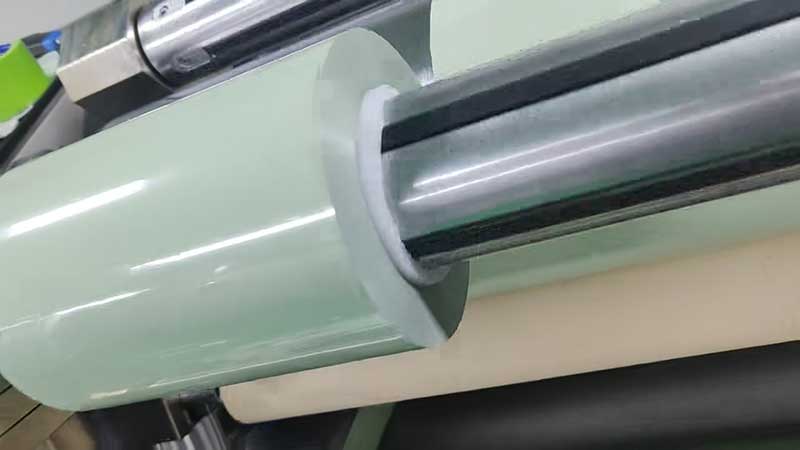
Film slitting machine solutions for packaging: material-based selection, blade matching, tension control tips to boost roll quality and efficiency.
21. November, 2026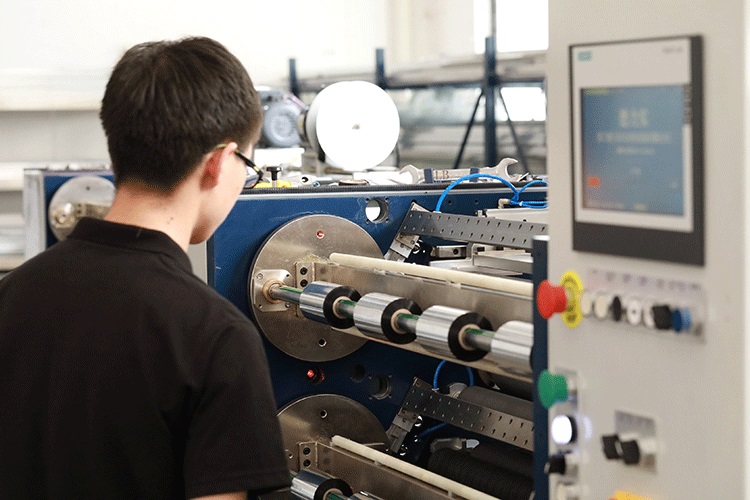
no need to buy a dedicated machine or gamble on a mismatched machine just because of a rushed resin-based washing order.
16. November, 2026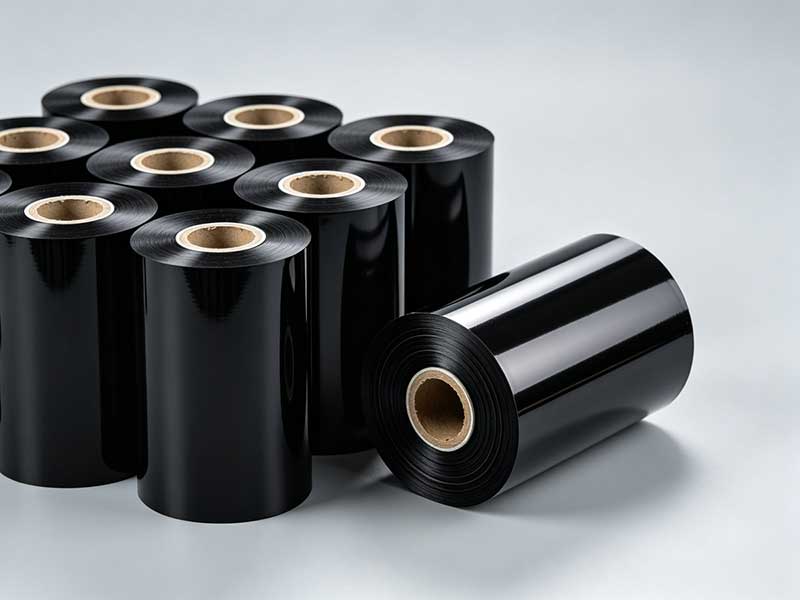
This article will start from symptom classification and provide a solution approach that progresses from simple to complex and can be quickly implemented.
16. November, 2026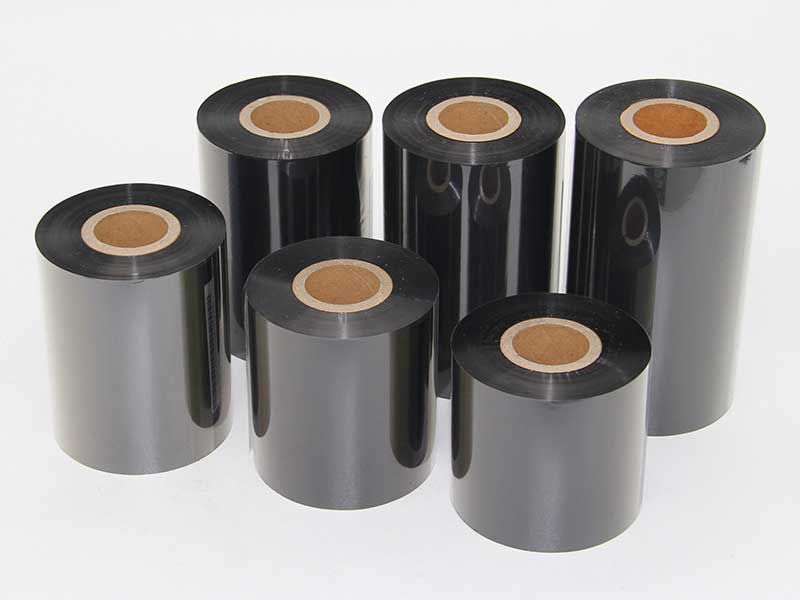
As a result, a well-calibrated high-precision ribbon slitting machine can stabilize width tolerances within ±0.05mm, and reduce the defect rate from 2% to 3% of ordinary equipment to below 0.3%.
16. November, 2026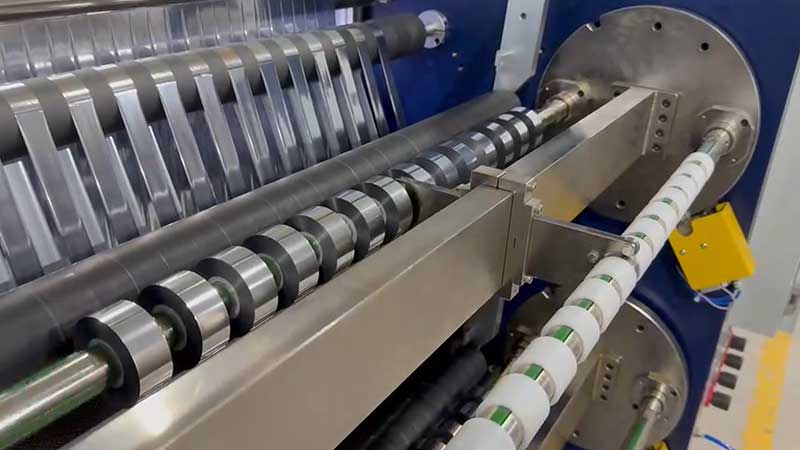
accuracy indicators will move from macro to micro, control logic will shift from experience to algorithms, and equipment roles will move from isolated islands to nodes.
10. November, 2026


 English
 Deutsch
 Français
 Español
 Português
 日本語
 русский
 한국어
 عربي
 ภาษาไทย
 Tiếng Việt
 Italiano